
WL-350D vs WL-350S vs WL-350DW: Which Label Printing Line Fits Your Job?
All three lines list a 350 mm maximum web width, but the artwork points to different equipment. The WL-350D UV has one screen-printing station and inline UV curing. The WL-350S has two screen stations. The WL-350DW combines registered screen printing with vertical cold foil. Each lists a 330 × 450 mm maximum print area and a 450 mm maximum feed length. Start with the layers the job needs, then check the proposed line against the actual roll.
Show what will be added to the label
Suppose a preprinted label needs an opaque white layer. The equipment team needs to see that layer and the printed feature it must align with. A second screen color changes the station sequence. Foil adds a transfer step and its own consumables. A finished-label photograph hides these differences, so send layered artwork with the existing print, each new screen layer, the foil area and registration reference marked. For foil work, include the proposed adhesive or transfer route.
Compare the listed configurations
The linked model pages provide the figures below. “Main machine length” describes the listed machine, not the space needed for the installed line. The layout also has to show unwinding, dryers, any foil equipment, rewinding and operator access.
| Model | Listed process | Curing equipment | Maximum web / print / feed | Listed main machine length |
|---|---|---|---|---|
| WL-350D UV | One screen color | Two-lamp UV dryer | 350 mm / 330 × 450 mm / 450 mm | 2500 mm |
| WL-350S | Two screen-printing stations | Two UV drying units, each with two lamps | 350 mm / 330 × 450 mm / 450 mm | 4300 mm |
| WL-350DW | Automatic registration, screen printing and vertical cold foil | Two-lamp UV dryer | 350 mm / 330 × 450 mm / 450 mm | 4300 mm |
The WL-350S adds a second screen station; the WL-350DW adds foil. Check the proposed sequence against the layered artwork before comparing prices. The catalogue gives no job-specific finished-label speed or guaranteed registration tolerance here. Those figures need a trial with your stock and a defined inspection method.
WL-350D UV: one screen layer and an inline cure
For one screen color, the WL-350D UV is the shortest of the three listed main machines. Its catalogue configuration runs from unwinding and feeding through one print station, a two-lamp UV dryer and rewinding. A dense white or varnish layer on a preprinted label also needs a clear registration reference. Show the earlier graphic it must meet and check how the proposed line will position it.
The ink, coating, liner and heat sensitivity need to be tested together on the production stock. If a second screen color is likely later, have the supplier draw that future line. The present one-station listing does not establish an upgrade path.
WL-350S: two screen colors in the same web path
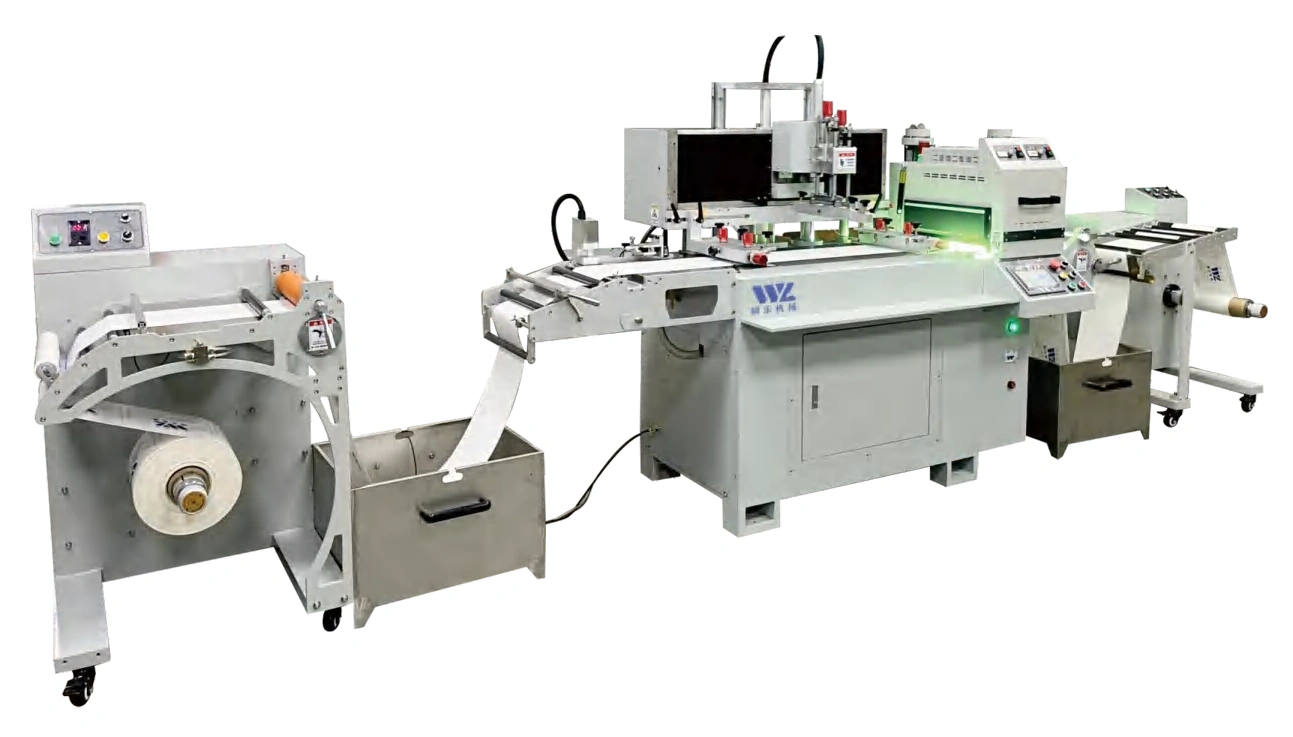
The WL-350S lists two printing stations and two UV drying units. It fits a job that genuinely needs two screen layers in the same web path. Put the layers in printing order on the artwork and identify what must cure before the web reaches the next station. On an already printed label, include the earlier flexographic or digital image in the registration plan.
Its listed main machine is 4300 mm long, compared with 2500 mm for the WL-350D UV. The catalogue lists 220 V for the main machine and a separate 380 V supply for the UV dryers. Use a complete line drawing and electrical schedule for installation planning; the main-machine dimension alone will leave out other equipment and working space.
WL-350DW: screen printing with vertical cold foil
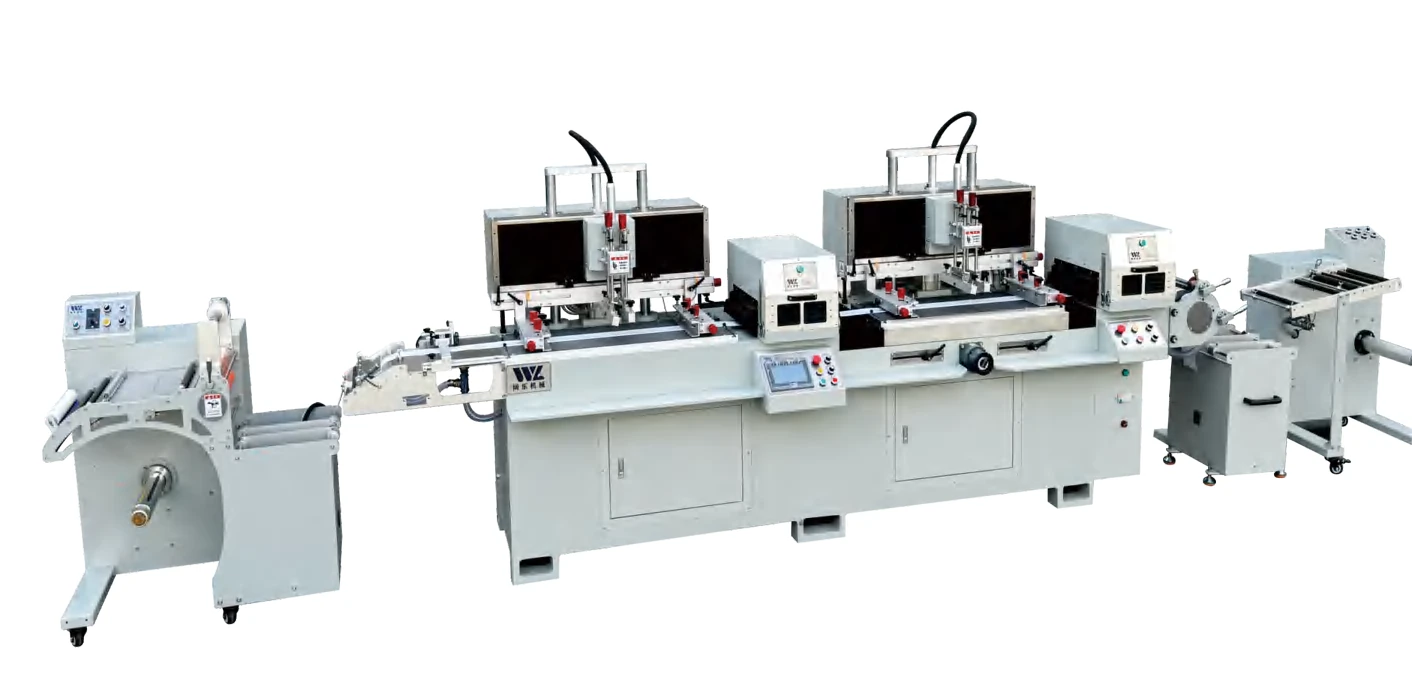
The WL-350DW brings screen printing and vertical cold foil into one listed configuration, with automatic registration and a two-lamp UV dryer. Consider it when the proposed workflow needs both the printed layer and metallic transfer. A metallic finished sample by itself says little about the machinery used to make it.
For a useful trial, provide the foil artwork, coverage, label stock, adhesive or ink, and print-to-foil alignment target. Bring a finished target sample and an unprinted production roll. Inspect the transfer and cure, then check the label again after rewinding or die cutting. If another line already handles the printing, compare a separate foil-finishing unit with the integrated route. The cold-foil planning guide goes into that choice.
Compare quotations against one job
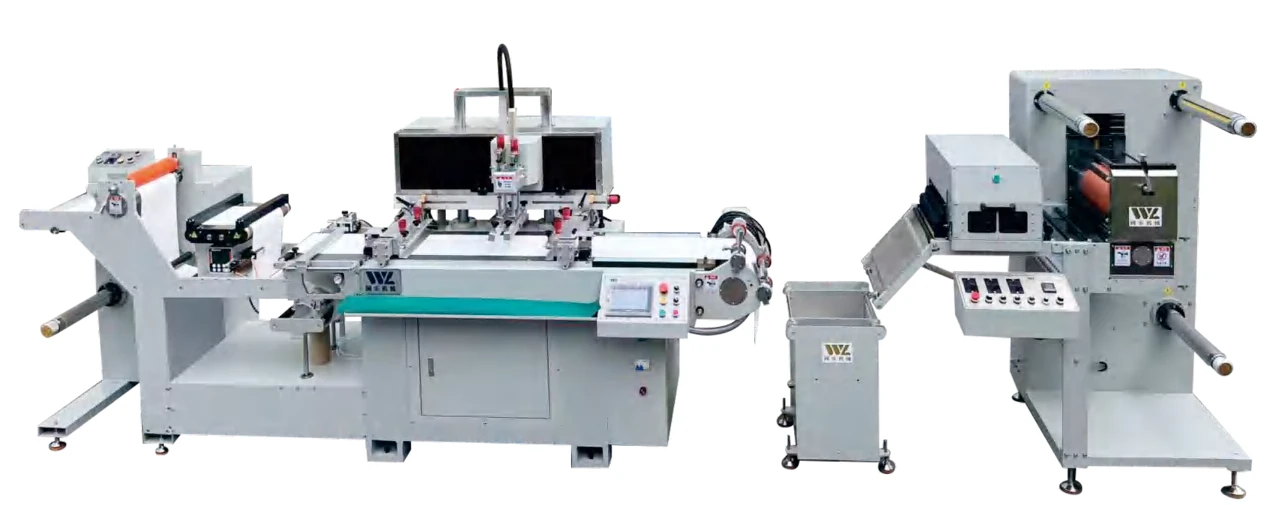
Give every supplier the same production roll, layered artwork and target label. The brief should state roll dimensions, image size, repeat length, screen layers, registration marks, ink or adhesive, curing limits, any foil area and the accepted output you need. The screen printing machine RFQ checklist has a fuller handoff template.
A comparable quotation names the supplied stations and dryers, feed direction, web guidance, electrical supplies, installation layout and trial conditions. Check edge clearance on the actual roll even when its nominal width is below the published maximum. Treat a catalogue rpm figure as a machine reference until a trial establishes accepted labels per hour for your job.
Questions that remain after the model comparison
Will a roll listed as 350 mm wide run on all three lines?
Each model lists 350 mm as its maximum web width. Guiding, edge position and registration marks still affect the usable path. Check a production roll and the artwork on the proposed configuration.
Does a second station make the WL-350S faster?
It adds a printing step, not a promised number of accepted labels per hour. Repeat length, stock, ink, curing and inspection set the practical output. Record those conditions in the trial.
What if the foil stage already exists elsewhere?
Show the current printer and finishing line on the layout. A separate foil unit may fit the job; compare web direction, registration, curing and rewinding before specifying an integrated line.
What belongs in the sample trial?
Use the production roll, layered artwork and a target finished label. Include the actual ink or adhesive and foil where relevant. Agree in advance on inspection after curing, rewinding and the next converting step.
Sources: the linked Winshol model pages and supplied 2026 equipment catalogue. The three machine photographs are from that catalogue. Confirm the final equipment scope, utilities and material acceptance criteria in the project quotation and sample test.
